
Two tubes exhibit the same Ra value of 0.4 µm each, measured with the same surface roughness tester, according to the same standard. Observed under an electron microscope, their profiles are completely different: one is regular, the other chaotic and sharp. In operation, they do not behave the same way.
Ra is the only value that most specifications require on a tube in the pharmaceutical industry. It is also the one that misleads the most people.
The controlled roughness of a pharmaceutical stainless steel tube is not a simple checkbox. It’s a combination of steel grade, manufacturing process, surface treatment, and a standard, chosen according to the fluid that will flow through it. Make a mistake on one element, and the rest of the specification is useless.
Ra (arithmetic mean roughness) is measured by palpation: a diamond point explores the surface, each vertical displacement is recorded, and the average of the deviations gives the Ra, according to the DIN EN ISO 4287 or ASME B46.1 standard.
The problem is that Ra is an average. It says nothing about the shape of the peaks, their density, or their distribution. Two surfaces can have the same Ra value of 0.5 µm with radically different topographies: one surface with fine, closely spaced peaks, the other with wide, deep troughs. The calculation gives the same result. The behavior in service does not.
This limitation has a concrete consequence on cleanability and corrosion resistance. A surface with a chaotic profile develops a real surface area significantly larger than its projected surface area: more material exposed to the fluid, more areas where a biofilm can develop, and more surface area to passivate. Conversely, an electropolished surface has a real surface area close to its projected surface area. This is why, for the same Ra value, an electropolished tube and a simply mechanically polished tube do not offer the same hygienic guarantee.
Ra remains the standard reference indicator, and it will continue to be required in your specifications. However, it should be interpreted as a minimum threshold, never as sufficient proof of a surface’s quality.
DIN 11866 doesn’t just specify diameters. It also classifies pipes by hygiene level, with a short code that says almost everything. H for hygienic. E for electropolished. A number for the maximum internal roughness: class 3, Ra ≤ 0.8 µm; class 4, Ra ≤ 0.4 µm; class 5, Ra ≤ 0.25 µm. And a lowercase “o” which, unlike the “o,” doesn’t refer to the internal surface: it indicates an external surface polished to Ra < 0.8 µm. We detail all these classes in our... article dedicated to the DIN 11866 standard.
At the house of DockweilerEach hygiene class corresponds to a specific tube reference:
| Classe d'hygiène DIN 11866 | Finition intérieure | Ra intérieur max. | Référence Dockweiler |
|---|---|---|---|
| H3o | Recuit brillant (BF) | 0,80 µm | Weldtron BF |
| HE3o | Électropoli (EP) | 0,60 µm | Weldtron EP |
| H4o | Recuit brillant (BF) | 0,40 µm | Safetron BF |
| HE5o | Électropoli (EP) | 0,25 µm | Safetron EP |
Two points to note. First, the Weldtron EP is classified HE30 but guarantees 0.6 µm, whereas Class 3 tolerates 0.8 µm: the manufacturer’s specification is more demanding than the threshold for its class. Second, both ranges are offered in 1.4435 BN2, with a delta ferrite content of 0.5% or less, including in the weld. The difference between Safetron and Weldtron lies in the roughness level: 0.40 µm for BF and 0.25 µm for EP, compared to 0.80 and 0.60 µm for Weldtron. Safetron is the range for the most critical fluids: EPPI, pure steam.
“DIN 11866 series A tube, class HE5o” is a complete specification, which the Safetron EP meets. “Polished stainless steel tube 0.25 µm” is not: neither the finish, nor the standard, nor the grade is fixed.
In the pharmaceutical industry, the internal roughness of a tube is specified fluid by fluid, not tube by tube. Here is the correspondence used in our facilities, compliant with GMP/BPF requirements:
| Fluide | Nuance | Surface intérieure | Tube Dockweiler (classe DIN 11866) |
|---|---|---|---|
| Eau prétraitée | 316L | Ra < 0,8 µm ou ASME BPE SF1 | Weldtron BF (H3o) |
| Eau pour préparations injectables (EPPI) | 1.4435 BN2 | Ra < 0,6 µm électropoli ou Ra < 0,4 µm non électropoli | Weldtron EP (HE3o) ou Safetron BF (H4o) |
| Vapeur pure | 1.4435 BN2 | Ra < 0,25 µm électropoli (éventuellement < 0,6 µm) | Safetron EP (HE5o), éventuellement Weldtron EP (HE3o) |
| Air procédé | 316L | Ra < 0,8 µm ou ASME BPE SF1, dégraissé oxygène | Weldtron BF (H3o) en ISO, TCC 0,8 µm en impérial |
| Skid process | 1.4435 BN2 | Ra < 0,4 µm ou ASME BPE SF4 | Safetron BF (H4o) |
One key point to remember: the more critical the fluid (pure steam versus pre-treated water), the more stringent the surface roughness requirements become, AND the harder the steel grade needs to be. Standard 316L is sufficient for low-criticality clean utilities. As soon as you’re dealing with EPPI (Electrical Pressure Equipment) or pure steam, you systematically switch to 1.4435 BN2, a European variant of 316L with a limited sulfur content, which is more stable for orbital welding.
The same logic applies to the entire process. The table below, taken from the materials/PREN reference document for pharmaceutical and biotech facilities, cross-references the corrosion resistance requirement (PREN, Pitting Resistance Equivalent Number) and the expected surface quality:
| Application | PREN requis | Qualité de surface |
|---|---|---|
| CIP | 20-25 | Poli mécanique / brillant |
| SIP | 20-25 | Électropoli |
| Eaux usées | 20-25 | Poli mécanique / brillant |
| WFI (eau pour injectables) | 20-26 | Électropoli |
| API par batch | 20-30 | Poli mécanique / brillant |
| API en continu | 20-45 | Poli mécanique / brillant / électropoli |
| Fermenteurs, vaccins, plasma sanguin | 25-40 | Électropoli |
The PREN is calculated using the formula PREN = %Cr + 3.3 × (%Mo + 0.5%W) + 16 × %N (ASME BPE 2022, Table F-3-1). The more a process operates in a chloride-rich environment at high temperature (fermentation, vaccines), the higher the required PREN, and the faster 316L reaches its limits in favor of 1.4435, 904L (UNS N08904) or AL-6XN.
316L (UNS S31603) is the most widely used material in pharmaceuticals: it offers a good compromise between corrosion resistance, ease of processing, and price. However, “316L” is an American designation with broad compositional limits. The European nomenclature is more precise: 1.4404 and 1.4435 are two equivalents of 316L, with 1.4435 containing more chromium and molybdenum, and therefore offering greater resistance to localized corrosion.
For hot fluids (above 60°C), the American designation 316L is no longer sufficient: it is necessary to specify 1.4435 BN2, a variant with limited sulfur content (S ≤ 0.015% recommended, practical acceptable difference between two components to be joined of approximately 0.007%). This limitation is not cosmetic: sulfur is a surfactant that influences the weld pool during welding, with a risk of arc deviation (Marangoni effect) specific to automatic orbital welding. A significant difference in sulfur content between two parts to be welded degrades the quality of the weld bead, regardless of any roughness specifications.
Beyond 1.4435, 1.4539 (904L) and AL-6XN come into play when the required PREN exceeds 30-40: fermentation, vaccines, blood plasma. These more alloyed grades, however, present specific welding challenges (ferrite content, sigma phase) that warrant a separate article.
A common misconception is that electropolishing “corrects” a surface. This is not what happens. Electropolishing removes material by preferentially eroding the peaks of the surface profile, depending on the duration and intensity of the electrochemical treatment. It does not recreate a perfectly smooth surface from any base, and it does not replace a prior mechanical polishing step if that step has left structural defects.
Comparing surface treatment processes yields a clear ranking in terms of surface area (and therefore cleanability), from least favorable to most favorable: raw mechanical polishing, cold rolling without mechanical polishing, pickling, and then electropolishing. Bare metal structures and polished or honed surfaces have an open structure that is difficult to clean. Pickling surfaces are clean but matte. Electropolished surfaces offer the best possible hygienic properties, provided that the initial surface condition before electropolishing is already satisfactory. Electropolishing improves a good substrate; it cannot compensate for a poor one. This is precisely the logic behind the HE classes of DIN 11866: a Safetron EP (HE50) is based on a Safetron substrate, not just any substrate.
These two references are often confused, even though they address different issues. LASME BPE (Bioprocessing Equipment) is a comprehensive design code: it covers materials, surface finishes (classes SF1 to SF6), welding, flow conditions, and the absence of dead legs. DIN 11866 is a tube manufacturing standard: it specifies dimensions (metric A series, ISO 1127 B series, imperial C series) and hygiene classes (H3 to H5 for bright annealed tubes, HE3 to HE5 for electropolished tubes).
A tube can therefore be manufactured according to DIN 11866 in class H4o (Safetron BF) and simultaneously meet a contractual requirement of ASME BPE SF1. The two standards describe the same surface with different limits: SF1 is capped at 0.51 µm, H4o at 0.40 µm. They are not interchangeable and cannot replace each other in a specification: ASME BPE qualifies the design of the entire installation, while DIN 11866 qualifies the tube. To learn more: our guide to the ASME BPE standard and its range of parts.
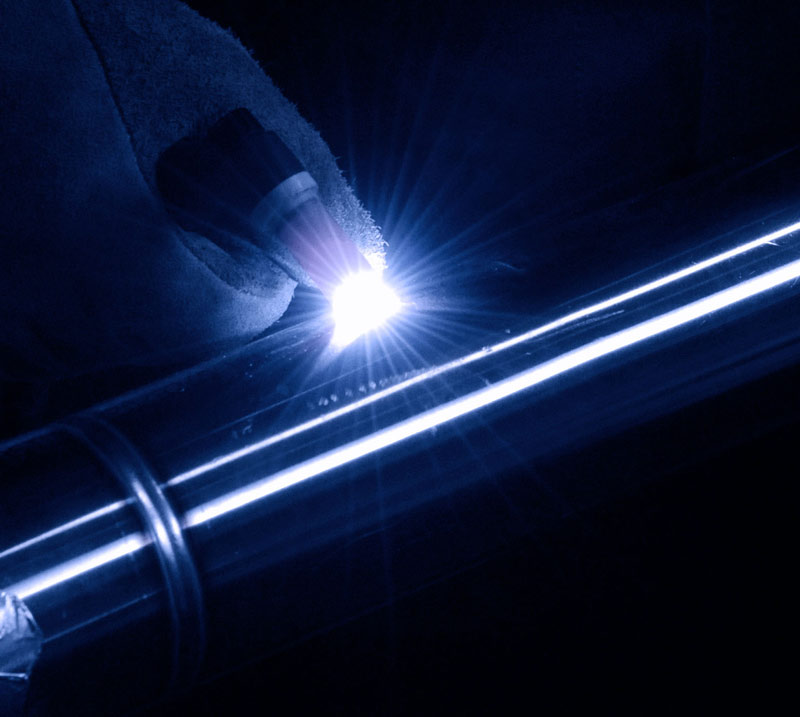
A tube with perfectly specified Ra can be ruined by a poorly executed weld. In pharmaceuticals, welds are by default all orbital, without filler metal, under U-grade argon. Manual welding is only tolerated in cases where it is physically impossible to position the orbital welding head.
The inspection covers precise tolerances: maximum over-thickness and concavity of 10% of the tube thickness (internal and external), bead alignment deviation limited to 35% of the thickness, and bead width increase limited to 50% of its smallest value. Non-penetration through the entire thickness is never acceptable.
The color of the weld bead inside the tube serves as a quick visual indicator of quality: only white and straw yellow are acceptable as is. Subsequent colors (blue, purple, gray, up to black) indicate increasing oxidation of the heat-affected zone, due to the presence of residual oxygen in the shielding gas. Once a certain color threshold is reached, the weld must be redone, regardless of the initial tube roughness. A Safetron EP classified as HE50 with a blue weld bead is no longer an HE50 tube.
Rouging is not a manufacturing defect, but a phenomenon that occurs during operation. It most often manifests in purified water or hot WFI loops, where the passive chromium film depletes locally over time due to the combined effects of temperature, water chemistry, and exposure time. Even a tube correctly specified in Ra and shade at the time of installation is not immune to rouging years later if the loop parameters (temperature, water quality, passivation frequency) are not controlled.
This is why post-weld chemical treatment is an integral part of the specification, just like Ra: degreasing with 2% sodium hydroxide for two hours for non-electropolished tubes, followed by passivation with 5 to 10% nitric acid (less than 20 ppm chloride), rinsing with demineralized water until the inlet/outlet delta is less than 1 µS/cm, and checking the pH to be close to neutral. Pickling, however, is excluded on clean fluid circuits, whether electropolished or not.
The most common mistake is to start with the dimensional standard or the Ra value to specify a tube. This is the reverse of the correct order:
Specifying in the other direction, that is to say choosing first a dimensional standard because that is what the supplier has in stock and then fitting an Ra to it, amounts to dressing up a need that has not yet been defined.
Ancien ingénieur mise en route et expert traitement d'eau dans un grand groupe alimentaire, puis chargé d'affaires en pharmaceutique, microélectronique et agroalimentaire. Profil LinkedIn
Dockweiler ranges in 1.4435 BN2, delta ferrite ≤ 0.5% including in the solder, distributed by Tubes Technologies, stock in Mions (69).
At Tubes Technologies, each pharmaceutical stainless steel tube roughness specification is built fluid by fluid, from the material/PREN matrices and the Weldtron (H3o, HE3o) and Safetron (H4o, HE5o) ranges of our partner Dockweiler.
 Article pilierASME BPE : ce que dit la norme, et toutes les pièces qui composent sa gammeLes 13 Parts de l'édition 2026 reliées à la gamme : matières, finitions SF1 à SF6, raccords, vannes.Lire l'article →
 NormeDIN 11866 : ce que dit vraiment la norme des tubes inox aseptiquesSéries A, B, C, classes H1 à HE5, suffixe « o », delta ferrite, pressions admissibles.Lire l'article →
 Glossaire visuelGlossaire visuel ASME BPE Part DT : la photo de chaque code32 codes Part DT en photo : coudes, tés, réductions, ferrules et bouchons, avec leur fiche produit.Lire l'article →